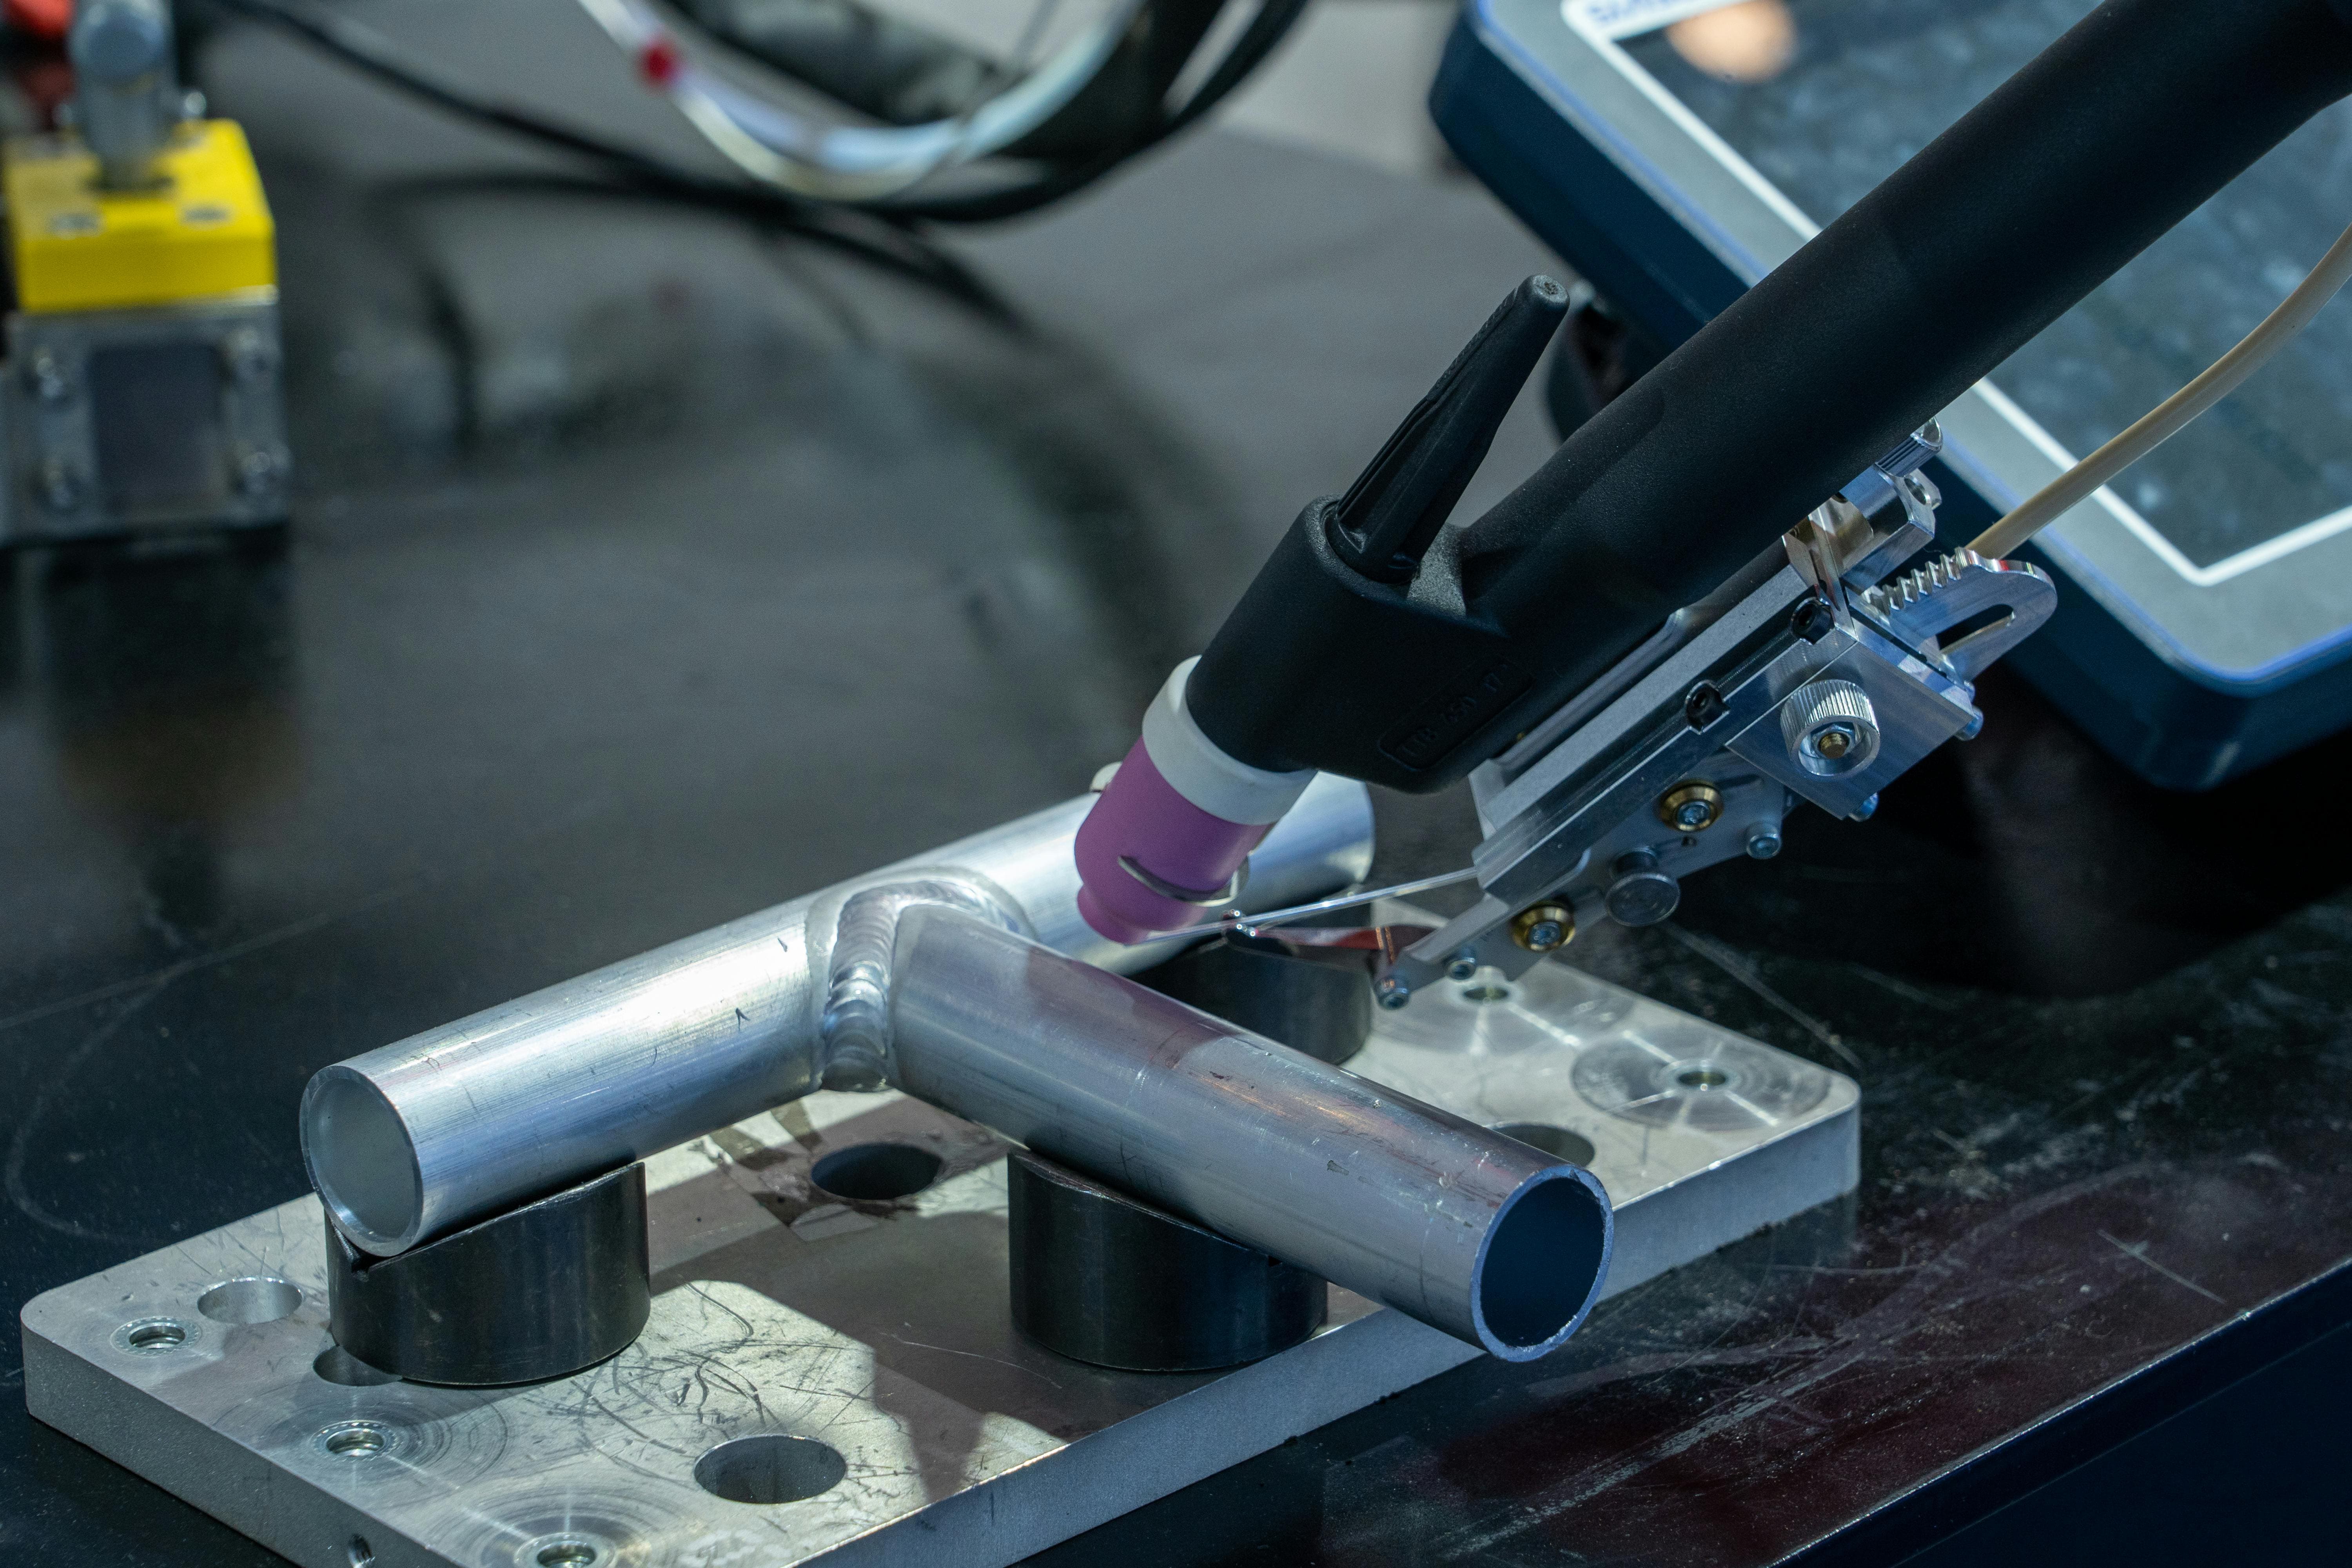
MIG, TIG and spot welded assemblies in mild steel, stainless and aluminium, made to qualified procedures by certified welders. WPS, welder certificates and NDT reports available with every order.
The process is chosen by material, thickness and how the weld will be seen or loaded. Specifying the wrong one either wastes money on finish nobody sees, or produces a joint that is not fit for its load.
Visible stainless welds on food or architectural equipment warrant TIG. A hidden structural frame in mild steel does not, and paying for TIG there is a common overspend.
A weld cannot be fully inspected by looking at it. Confidence comes from qualified procedures and welders, and from testing matched to how critical the joint is.
For structural, pressure or load-bearing assemblies, ask for the WPS and welder qualifications with the quotation. For EU structural work, EN 1090 execution class determines what is required.
Welding heat makes metal expand and contract, pulling assemblies out of shape. Controlling it is a design and sequencing problem as much as a welding one.
If an assembly has tight flatness or hole-position requirements, critical features are usually machined after welding rather than before.
On specifications: the capabilities above reflect standard specifications for this process. Achievable tolerances and finishes for your part depend on geometry, material and quantity, and are confirmed at quotation after drawing review. Every first article ships with a full dimensional inspection report against your drawing, plus Material Test Certificates for the raw material. We do not ask buyers to take a capability claim on trust.
Welded assemblies ship with the records that prove the weld, not just the dimensions.
HS Code 7308 (structures) · 7326.90 (other steel articles) · 7610 (aluminium structures). Confirmed at order stage.
MOQ is discussed at order stage based on part complexity and material. Payment by advance TT, LC at sight, or DP/DA case by case.
Choose by material, thickness and visibility. MIG suits mild steel frames and volume work. TIG suits stainless, aluminium, thin sections and visible welds. Spot welding suits sheet metal lap joints. Paying for TIG on a hidden mild steel frame is a common overspend.
Through qualified procedures and welders plus testing matched to how critical the joint is. A written WPS backed by a PQR proves the procedure works, welders are certified to ISO 9606 or ASME IX, and every weld is visually inspected. Critical joints can be checked by ultrasonic, radiographic, magnetic particle or dye penetrant testing.
A quality framework for fusion welding manufacturers, covering procedures, personnel, equipment, inspection and records. It is commonly referenced in European structural and pressure work, and is tied to EN 1090 execution classes for structural steel.
Through balanced weld sequences, fixtures that hold geometry during welding and cooling, minimum necessary weld size, and intermittent welds where full-length welds are not needed. Where flatness or hole positions are critical, those features are machined after welding.
Yes. Stainless assemblies can be pickled and passivated to restore corrosion resistance at the welds, and steel assemblies powder coated or hot-dip galvanised. Stress relief heat treatment is available for assemblies that need dimensional stability.
Steel structures and parts of structures fall under HS Code 7308, other welded steel articles under 7326.90, and aluminium structures under 7610. The correct code is confirmed at order stage based on the assembly and its end use.
Technical drawings welcome. FOB or CIF pricing within 24 hours. Third-party inspection available.
Technical drawings welcome. FOB or CIF pricing, samples available.
Request Quote → 💬 WhatsApp +91-9066444896