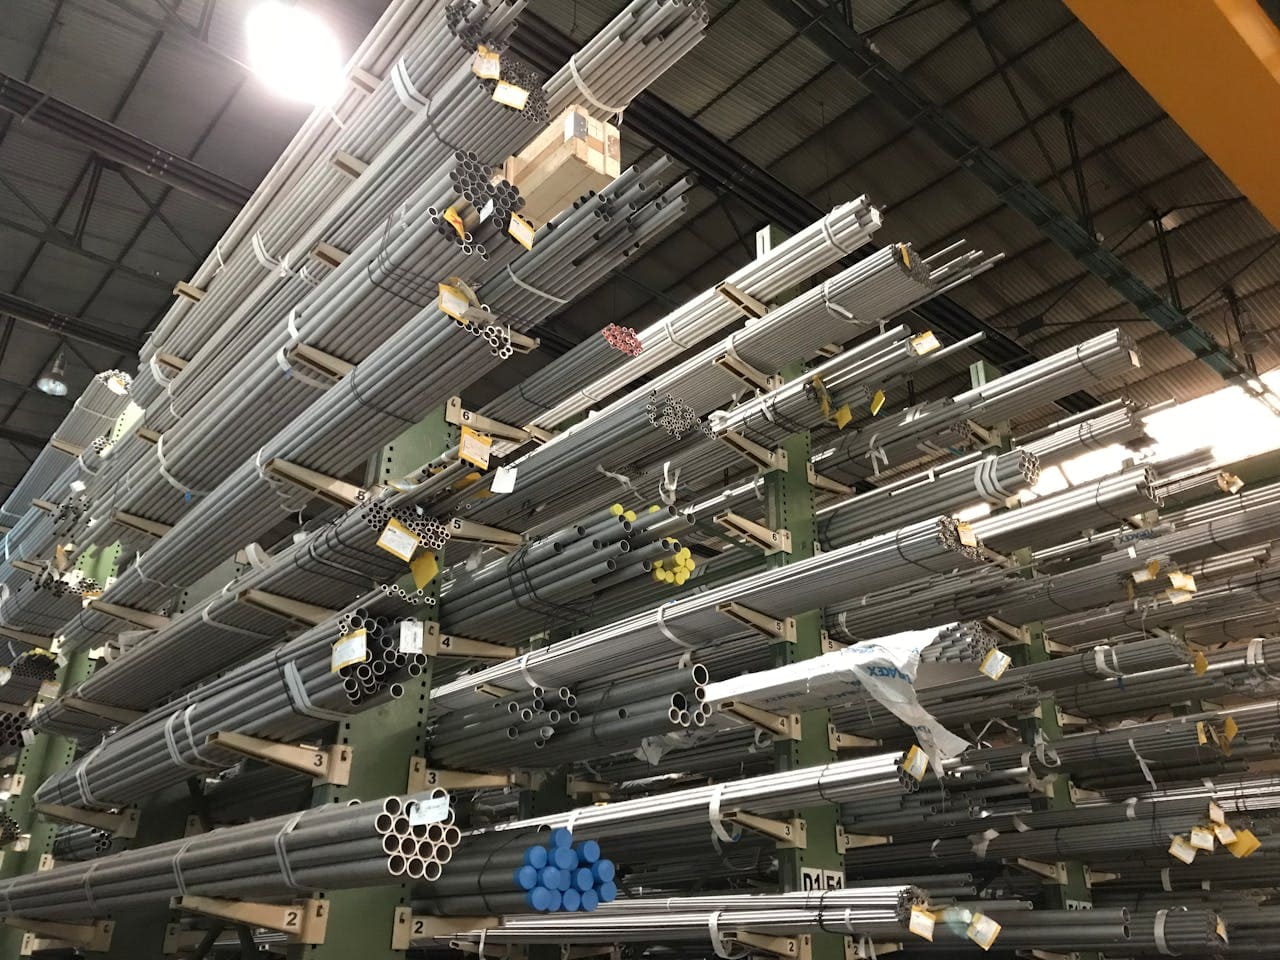
SS 304 and low-carbon 304L in sheets, plates, coils, pipes and bars to ASTM A240 and EN 10088. Finishes 2B, BA, No.4 and No.8, with Mill Test Certificate traceable by heat number on every shipment.
SS 304 and 304L are the same alloy with different carbon limits. That single difference decides whether your welded joints survive corrosive service, and it is the most common specification error on stainless orders.
If your part is welded and then goes into a corrosive environment, specify 304L. Sensitisation happens when carbon forms chromium carbides at grain boundaries during welding, stripping chromium from the surrounding metal and leaving it vulnerable to intergranular corrosion. Low carbon prevents it.
Finish affects appearance, cleanability and corrosion behaviour. Stating "polished" or "bright" is not a specification — use the standard codes.
For food and pharmaceutical equipment, No.4 or BA are normal because a smoother surface harbours less bacteria and cleans more easily. 2B is the mill standard and correct for most general fabrication.
On specifications: the figures above reflect standard industry specifications for this product. Your actual batch values are confirmed on a NABL-accredited Certificate of Analysis issued against your specific lot — provided with every shipment, and with sample orders before you commit to bulk. We do not ask buyers to take a specification on trust.
Mill Test Certificate is provided with every shipment, traceable by heat number to the specific material supplied.
For stainless steel the Mill Test Certificate is the only meaningful verification — visual inspection tells you nothing about chemistry.
HS Code 7219 (flat, width 600mm+) · 7220 (flat, under 600mm) · 7222 (bars). PMI verification available on request.
MOQ is discussed at order stage based on form and dimensions. Payment by advance TT, LC at sight, or DP/DA case by case.
The carbon limit. 304 allows up to 0.08 percent carbon; 304L is restricted to 0.03 percent. During welding, carbon forms chromium carbides at grain boundaries, stripping chromium from the surrounding metal and leaving it open to intergranular corrosion. That process is called sensitisation. If your part is welded and then enters corrosive service, specify 304L.
Use the standard code, not a description. 2B is the smooth mill finish and the correct default for general fabrication. BA is bright annealed and near-mirror, used for architectural and hygiene-critical work. No.4 is a uniform brushed satin, standard for food equipment and appliances. No.1 is hot rolled annealed, used where appearance does not matter.
It refers to the nominal composition: approximately 18 percent chromium and 8 percent nickel. Chromium forms the passive oxide layer that gives stainless its corrosion resistance; nickel stabilises the austenitic structure, which is what makes 304 formable and non-magnetic in the annealed condition.
Flat-rolled stainless products 600mm wide and above fall under HS Code 7219; below 600mm under 7220. Bars and rods fall under 7222, seamless pipes under 7304 and welded pipes under 7306. We declare the correct code based on the form ordered.
Yes, with every shipment. For stainless steel the MTC is the only meaningful verification, since visual inspection tells you nothing about chemistry. It shows heat number, full chemical analysis and mechanical test results against ASTM A240 or the applicable EN standard. For EU pressure applications an EN 10204 3.1 inspector-signed certificate is available on request.
Yes. Third-party pre-shipment inspection by SGS, Bureau Veritas or Intertek is available on request, and Positive Material Identification by XRF can confirm grade on the physical material. Both are worth arranging on first transactions and for critical applications.
Technical drawings welcome. FOB or CIF pricing within 24 hours. Third-party inspection available.
Technical drawings welcome. FOB or CIF pricing, samples available.
Request Quote → 💬 WhatsApp +91-9066444896